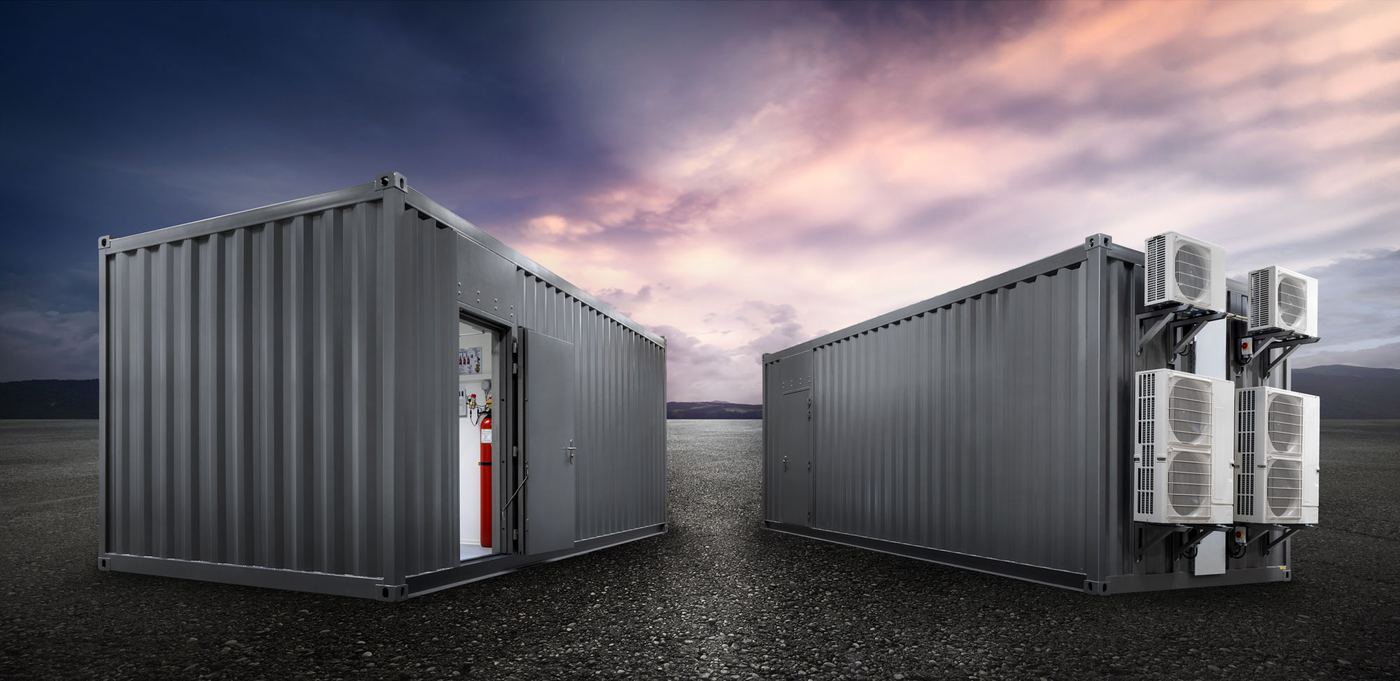
Specialised steel enclosures
Specialised enclosures and E-houses. Steel to finished enclosure, under one roof.
BESS · data centre gensets · diesel & gas gensets · compact substations. Built on robotic welding, an ISO 12944 C5M paint system and precision pneumatic jigs.
Robotic & semi-automated welding
Repeatable structural welds, with procedures engineered to EN 1090 / ISO 3834.
C5M marine-grade paint system
ISO 12944 C5M high-corrosivity coating system, applied and cured in a dedicated booth.
BESS
Data centre gensets
Diesel & gas gensets
Compact substations
One envelope, three disciplines — steel shell, structural weldment and electrical provisions, under one roof.
Steel to finished enclosure
Watch an enclosure come together.
-
00 / 06
Steel intake
Every enclosure starts as plate and section steel, drawn in to one plant.
-
01 / 06
Base frame
Bottom rails and cross-members are cut and fixed in precision jigs first, so the footprint starts square.
-
02 / 06
Corner posts and castings
ISO-format posts and corner castings lock the footprint. Engineered to ISO 1496-1; type approval in progress.
-
03 / 06
Corrugated shell
Corrugated walls add stiffness without added weight, welded on procedures engineered to EN 1090 / ISO 3834.
-
04 / 06
Roof and door end
Roof panels, door leaves, hinges and locking bars come off jigs built to Powervault drawings, so they fit first time.
-
05 / 06
Fit-out
Cooling units, cable gland plate, fire suppression and electrical provisions go in under the same roof.
-
06 / 06
C5M finish
ISO 12944 C5M coating system, applied and cured in a dedicated booth. Finished enclosure, ready for the yard.
Send an enquiry
- Steel intake. Every enclosure starts as plate and section steel, drawn in to one plant.
- Base frame. Bottom rails and cross-members are cut and fixed in precision jigs first, so the footprint starts square.
- Corner posts and castings. ISO-format posts and corner castings lock the footprint. Engineered to ISO 1496-1; type approval in progress.
- Corrugated shell. Corrugated walls add stiffness without added weight, welded on procedures engineered to EN 1090 / ISO 3834.
- Roof and door end. Roof panels, door leaves, hinges and locking bars come off jigs built to Powervault drawings, so they fit first time.
- Fit-out. Cooling units, cable gland plate, fire suppression and electrical provisions go in under the same roof.
- C5M finish. ISO 12944 C5M coating system, applied and cured in a dedicated booth. Finished enclosure, ready for the yard.
What we build
Four enclosure families, engineered as one discipline.
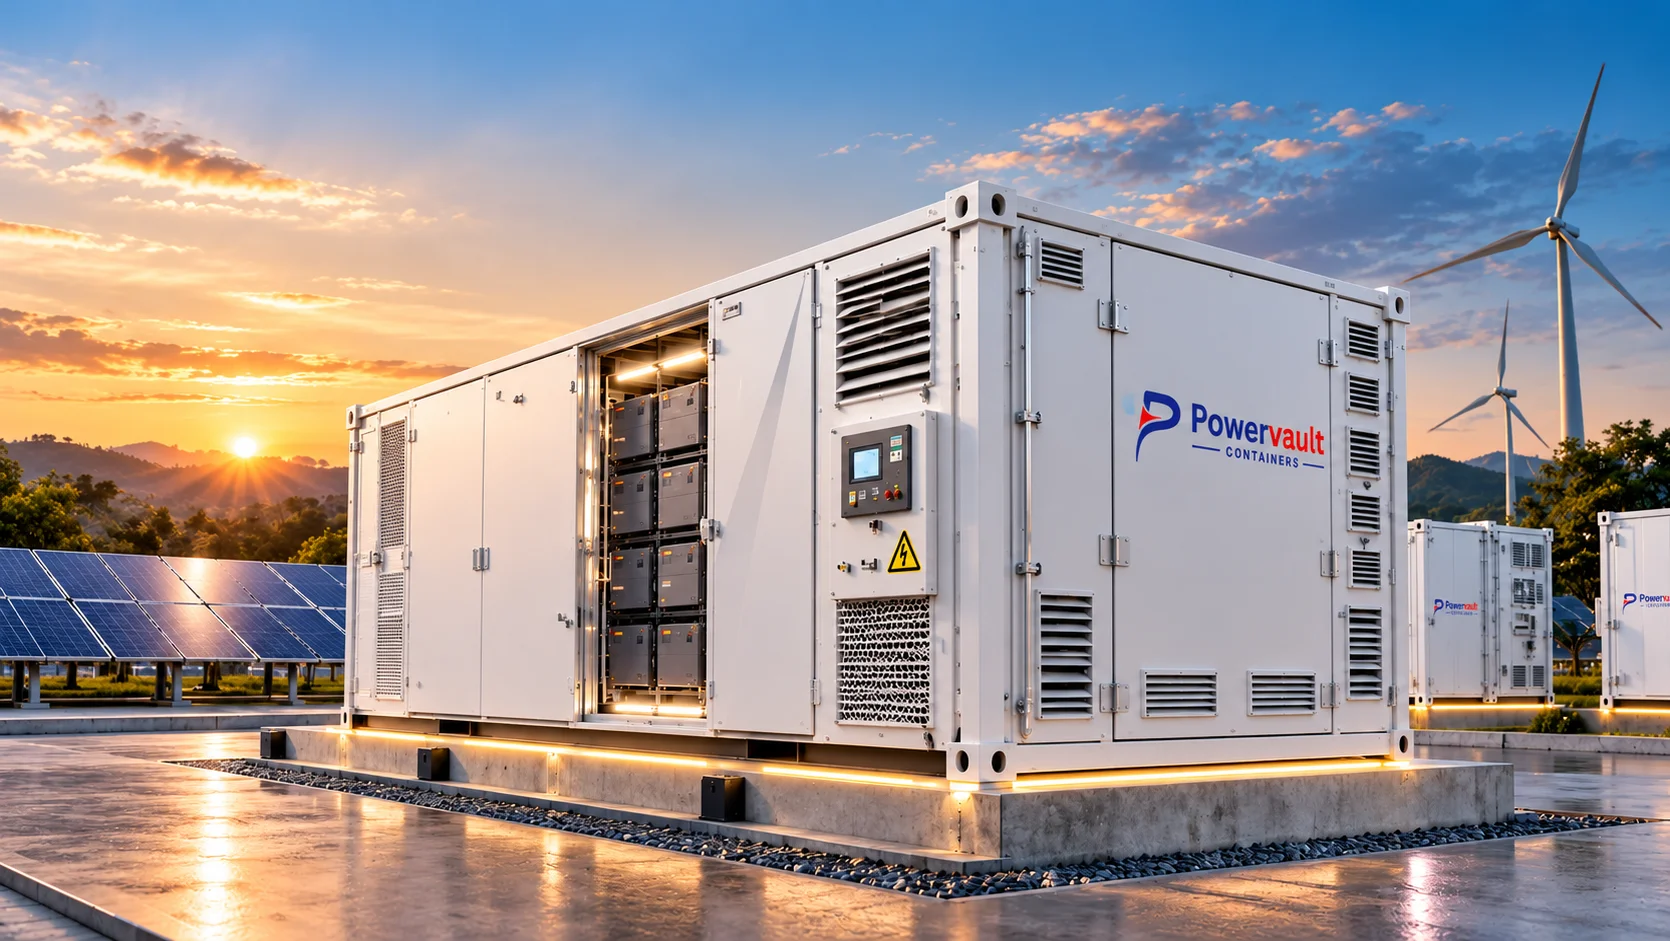
BESS enclosures
Battery energy storage enclosures built to survive thermal, fire and duty-cycle demands over a multi-year field life.
View enclosure →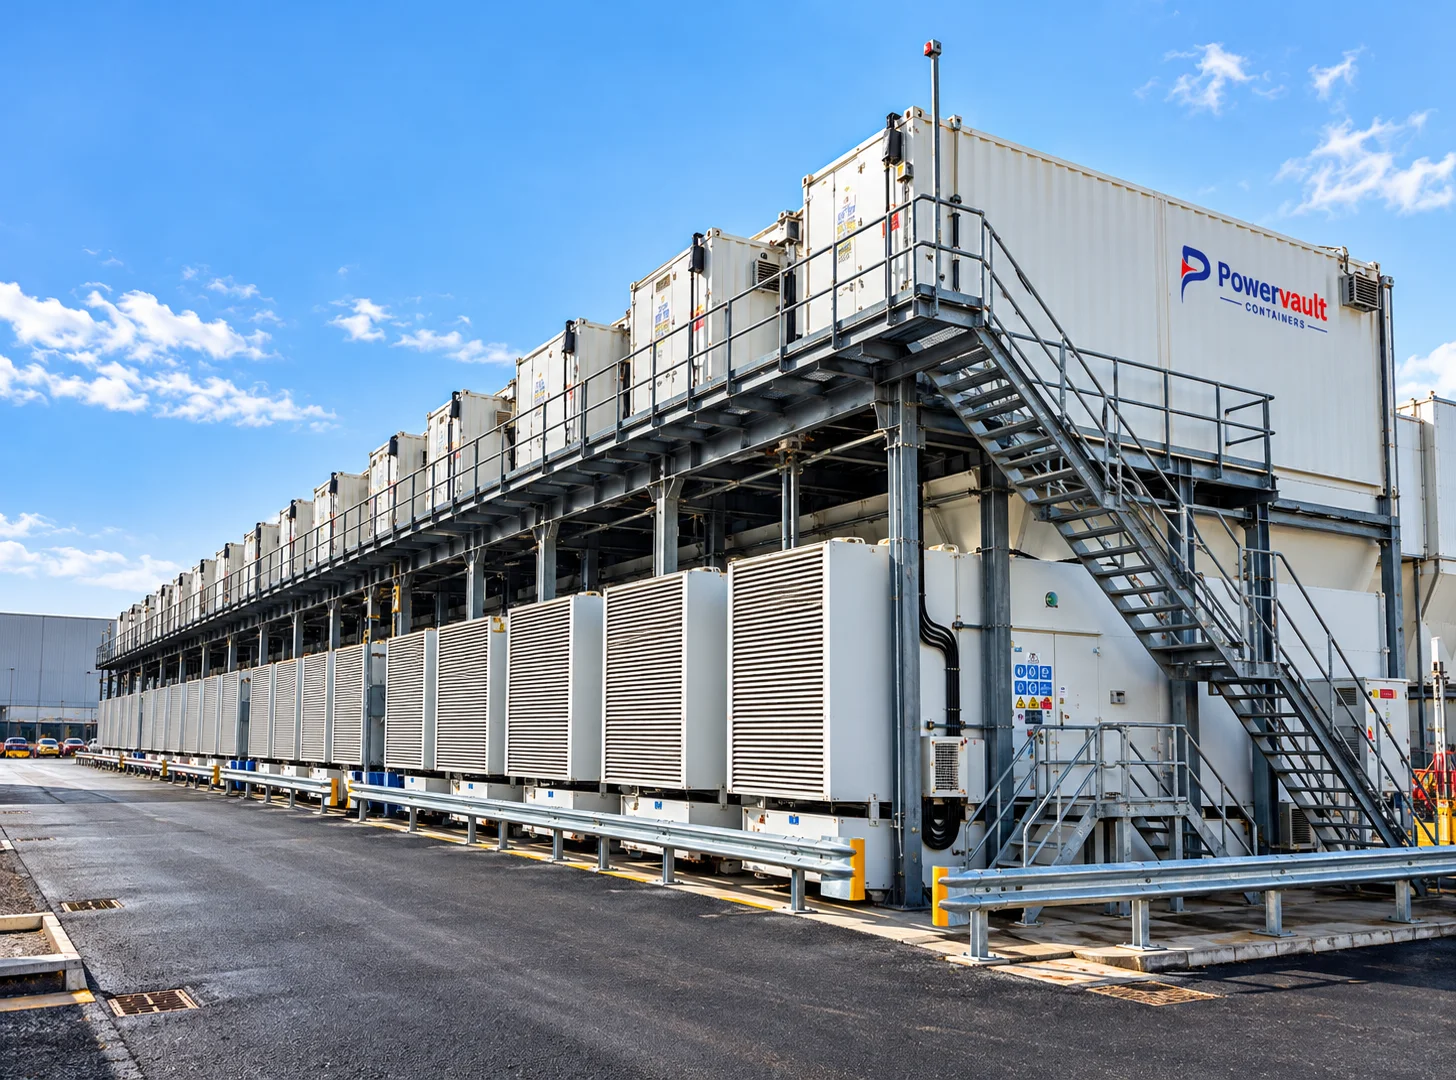
Data centre genset enclosures
Genset enclosures engineered against the acoustic and availability specification set by the facility.
View enclosure →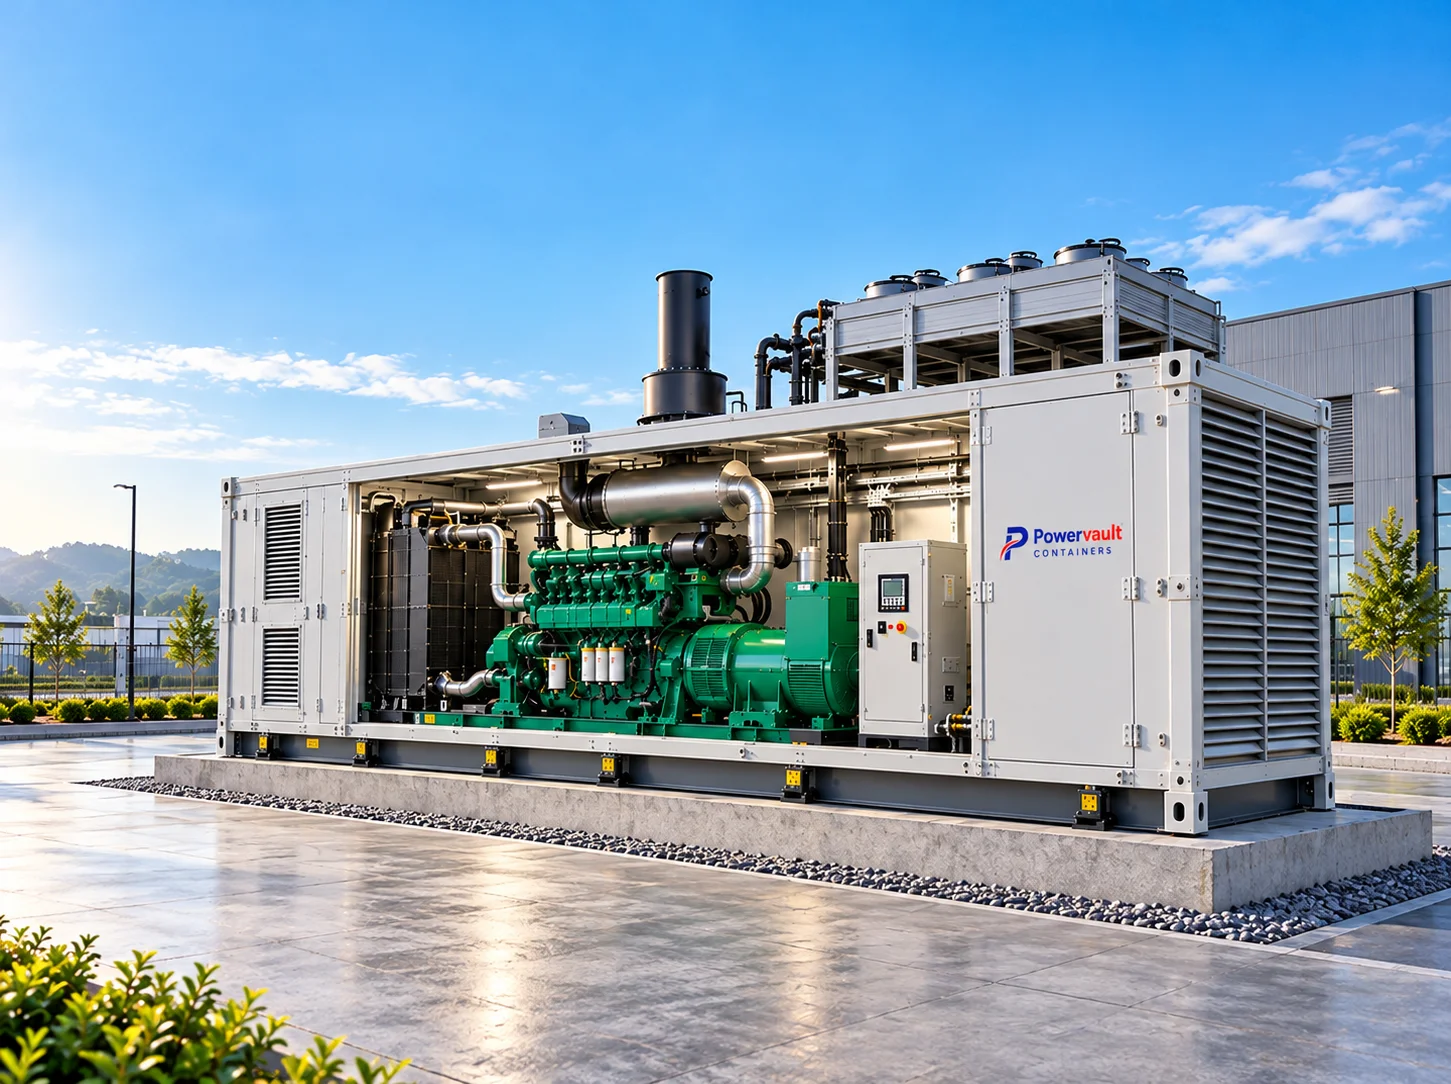
Diesel & gas genset enclosures
Acoustic genset enclosures for standby and prime power, sized and finished to the site they will stand in.
View enclosure →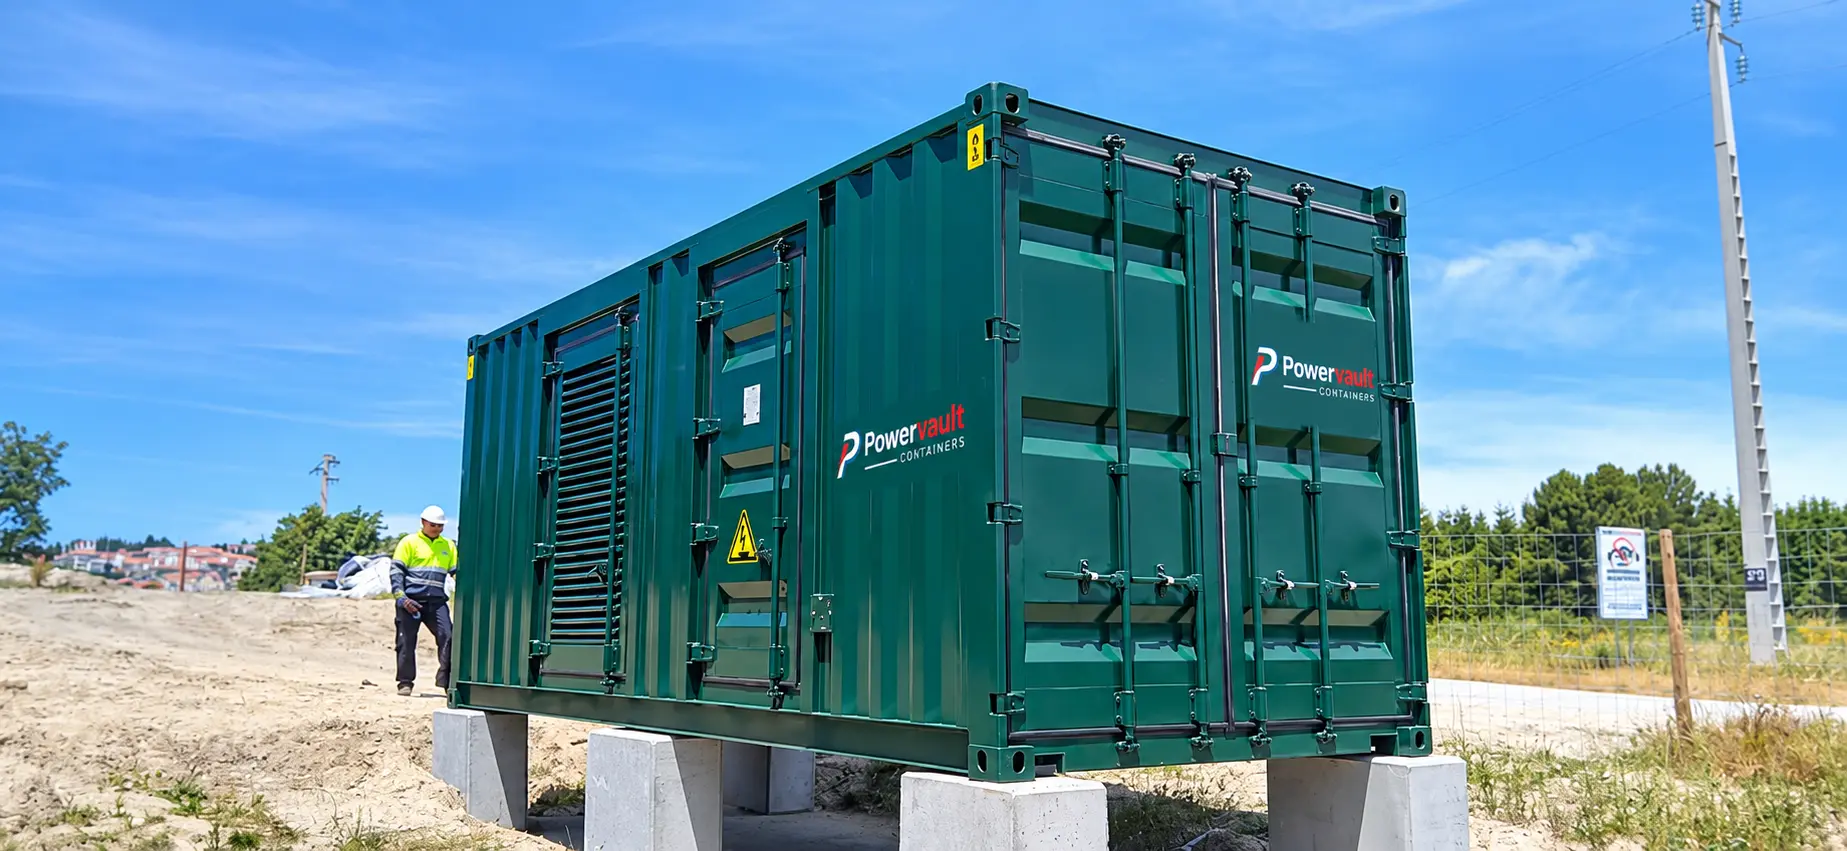
Compact substation & E-house enclosures
Switchgear and transformer enclosures built for utility and industrial deployment, documented for empanelment.
View enclosure →
Why the process matters
Four things we control in-house.
01
Steel-to-finished, in-house
Full process control and traceability from incoming steel to painted, tested enclosure. No sub-contracted quality gaps, and one point of accountability for schedule.
02
Robotic & semi-automated welding
Repeatable structural welds, with procedures engineered to EN 1090 / ISO 3834 — not job-shop hand welding. Weld quality is one of the leading causes of field failure in steel enclosures.
03
C5M marine-grade paint system
ISO 12944 C5M high-corrosivity coating system, applied and cured in a dedicated booth. Coastal and industrial sites quickly expose an under-specified coating.
04
Precision jigs & fixtures
Customisable pneumatic jigs, designed to Powervault drawings, for dimensional accuracy and interchangeability. Doors, glands and equipment fit first time on site, and replacement parts are interchangeable.
Current projects
The products we are currently making.
These are currently under design and execution.
Genset enclosures
Containerised data-centre genset enclosures for two leading global genset OEMs.
View enclosure →1250 kVA powerpack
A containerised powerpack in a 20 ft enclosure for the Middle East market.
View enclosure →CSS enclosures
Export-ready containerised substation enclosures, in 20 ft and 40 ft designs, for renewable energy companies.
View enclosure →
40+
years of European power-enclosure design experience
Design partnership
Engineered with European design pioneers.
We have tied up with European designers who have been in the business of making power enclosures for over 40 years, and who are among the pioneers in the field. Their engineering and vast experience go into every Powervault design.
Already proven. The first few projects we have worked on have saved customers space and cost.
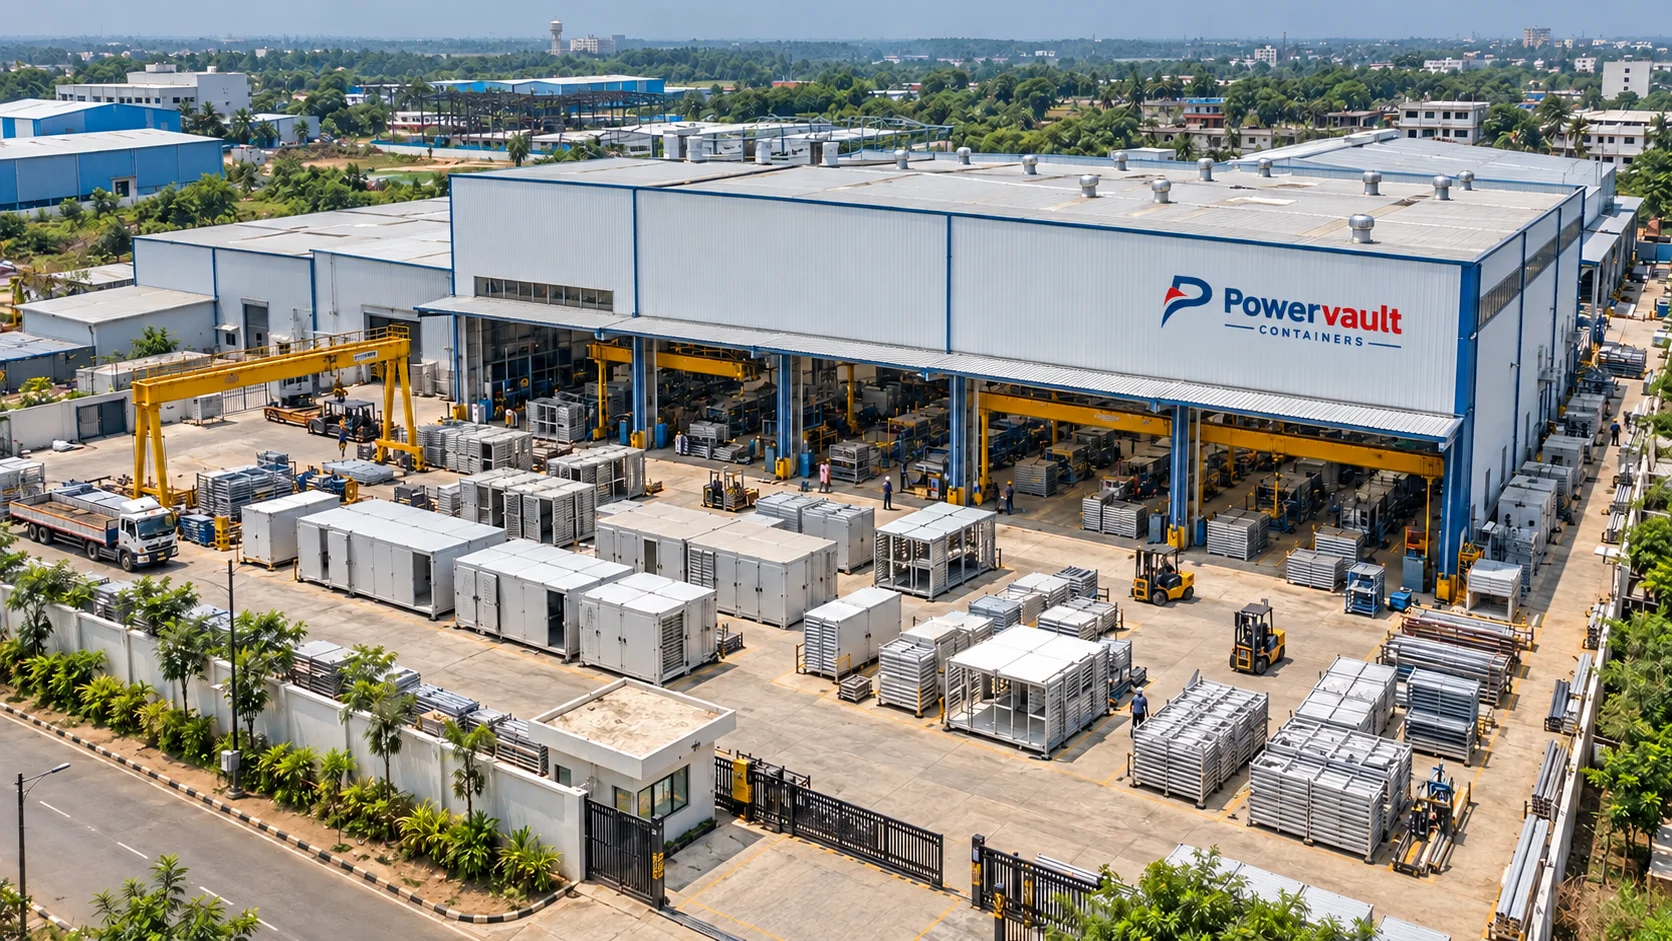
Production line
From coil to dispatch.
Twelve controlled stages, from incoming steel coil to customer inspection and dispatch.
01
Decoiling
Steel coil is received to specification and unwound into flat sheet, traceable by heat number.
02
Slitting and cutting
Coil is slit and cut to the exact sizes required for each part of the container.
03
Sheet blasting and primer
Sheet is blasted and primed to 25 µm, the primer thickness limit that still allows clean welding.
04
Shearing, notching and forming
Shearing, notching and press brakes form the sheet into the finished components.
05
Sub-assembly
Every weldment is held in a fixture, so dimensional accuracy is maintained from the first sub-assembly.
06
Main assembly
The complete enclosure is welded in fixtures, with robotics at every station where it is feasible. Procedures developed to EN 1090 / ISO 3834.
07
Blasting
The assembled enclosure is blasted to the surface standard the coating system requires.
08
Auto painting
The ISO 12944 C5M coating system, applied and oven-cured in a dedicated booth.
09
CSC testing
Structural and water-ingress testing before the enclosure leaves the line. ISO 1496-1 type approval in progress.
10
Fit-out
Internal systems and fittings installed to the customer’s specification.
11
Customer inspection
Your team inspects and signs off the finished unit at our works.
12
Dispatch
Final documentation, packing and loading for transport.
~10 acres
Site area
~16,000 m²
Factory floor area
Built to scale. The plant is laid out for specialised enclosures and E-houses, with floor space reserved for added capacity as demand grows.
Standards & quality
Engineered to. Not implied.
What we engineer to, and where each item genuinely stands today.
| Standard | Scope | Status |
|---|---|---|
| ISO 668 / ISO 1496 | Dimensions, ratings and structural testing (ISO Series 1 format) | Engineered to — ISO 1496-1 type approval in progress |
| EN 1090 / ISO 3834 | Structural steelwork and welding quality | Engineered to — certification planned |
| ISO 5817 / ISO 9606 | Weld quality levels and welder qualification | Engineered to — welder qualification to ISO 9606 at plant start-up |
| ISO 12944 C5M | High-corrosivity marine coating system | Engineered to — coating system per paint supplier's C5M specification |
| ISO 1461 | Hot-dip galvanizing | Specified where required — by approved galvanizer |
| IS 800 / IS 2062 | Indian structural steel design and material | Engineered to |
| IEC 61439 | Low-voltage switchgear and controlgear assemblies — enclosure provisions, where housed | Engineered to |
| IEC 62619 | Safety of secondary lithium cells and batteries | Customer scope — cell and battery-system certification sits with the integrator |
| IEC 62933 | Electrical energy storage systems | Design reference — enclosure requirements addressed; system compliance with integrator |
| UL 9540 / NFPA 855 | ESS safety and installation context | Design reference — system listing with integrator |
| IEC 62271-202 | High-voltage / low-voltage prefabricated substations | Engineered to — type test per customer requirement |
Certification scope is confirmed per customer requirement at order stage.
Get a technical response
Send us a specification and we will come back with a technical response.
Application, sizing, coating grade and governing standard — the more you give us, the faster we can price it.